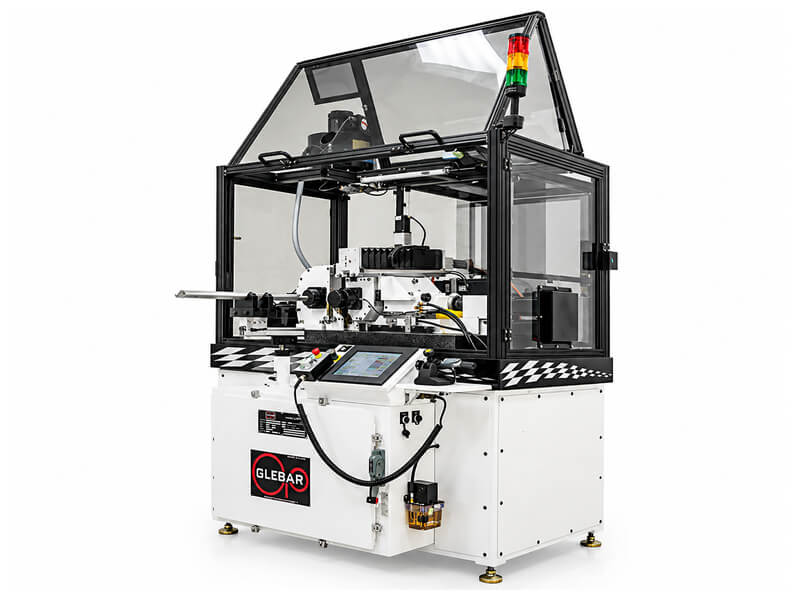
Arthroscopic Shavers – Inner Tube | Glebar GT-610 CNC
Challenge
The challenge was to develop a customized grinding solution that could process two mating metal components with tight surface clearance while meeting the precise manufacturing requirements of a powered arthroscopic shaver for orthopedic joint surgery.
Process
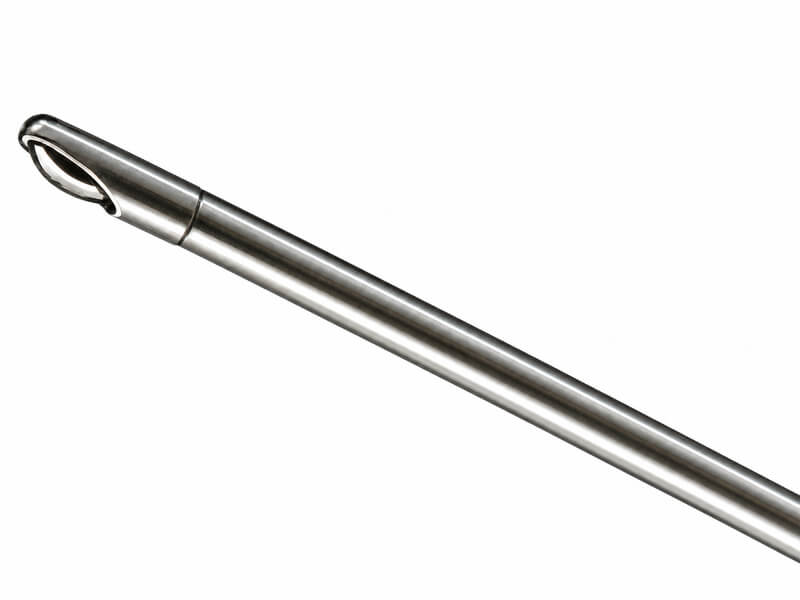
In this application, two tubes are assembled with a minimal gap between them—sometimes as small as 0.0005 inches. This allows the inner tube to move freely within the outer tube while preventing debris from getting trapped between the surfaces. The tips of the tubes typically feature a rounded guiding surface, while the outer tube has a window cut into it to expose the inner tube’s sharp edges.
Using MMT’s Glebar GT‐610 CNC Centerless Grinder to infeed grind the shape of the inner tube, a +/‐ 0.0002” tolerance was maintained on the tip dimensions. In addition, 3 diameter features were ground to within 0.0002” per diameter, maintaining a TIR of 0.0001” and producing a smooth 9 Ra surface finish on 304V stainless steel with a +/‐0.001” wall thickness. Removed were 0.012” in stock for the majority of the part and 0.004” from the tip geometry. The updated, fully automated process now completes in less than 20 seconds and adjusts for part-length variation, thermal expansion, and a near-zero tip-geometry requirement.
Solution
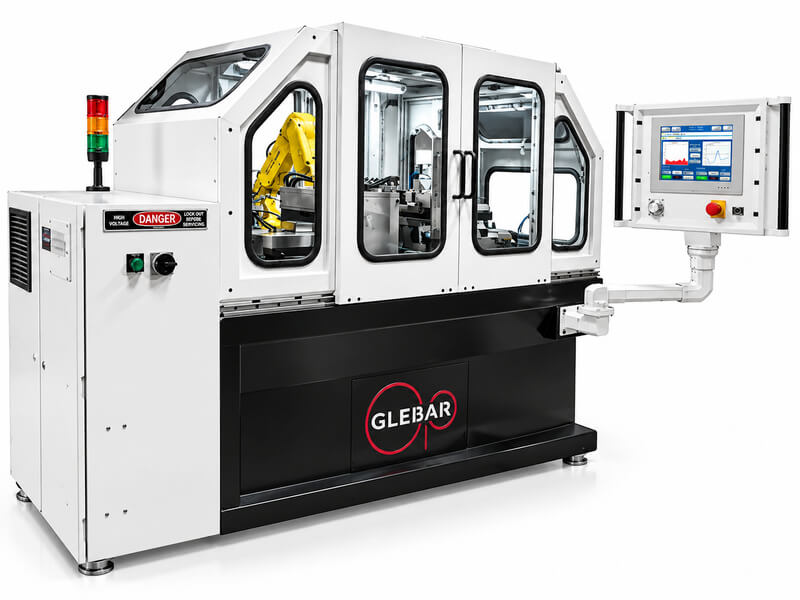
Using the Glebar GT-610 CNC High Precision Automated Infeed/Thrufeed Centerless Grinding Machine, MMT engineered a tailored process that maintained a +/- 0.0002 in tolerance on tip dimensions while providing the minimum gap between assembled parts needed to prevent debris accumulation between surfaces. The optimized process was completed in under 20 seconds per part, significantly reducing previous scrap rates.
Contact an EngineerResults
This solution significantly reduced scrap rates caused by tip-geometry imperfections and eliminated an extra step in the previous manufacturing method that left unacceptable surface tool marks. For the outer sleeve, the Glebar GT‐610 Thrufeed Grinder ground the blank tubes’ OD, maintaining a surface finish of 3‐6 RMS and a comfortable 2‐3 Cpk on the outside part diameter. The fully automated turnkey process easily met a material removal of 0.005” with a tolerance requirement of ±0.0005”.