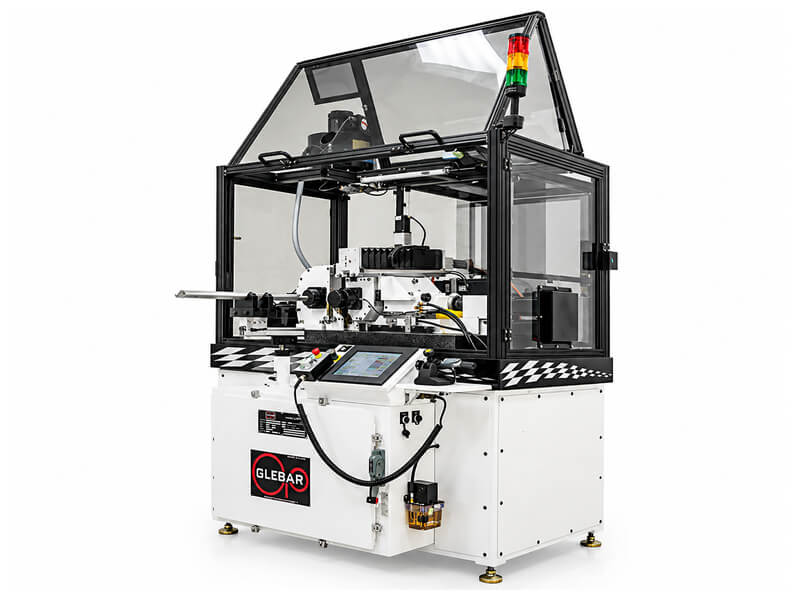
Filler Spouts | Glebar GT-610 Centerless Grinder
Challenge
A food equipment manufacturer approached Glebar to improve productivity and reduce costs for its food filler machines. The metal spouts in these machines require precision grinding for several critical reasons: they contact food directly, demanding a smooth surface finish for sanitary compliance, and they must mate closely with their housing to maintain the pressure needed to dispense precise quantities without leaking. Spouts are also frequently exchanged to accommodate various pastry sizes, making rapid changeover between components an important production consideration.
The project involved eight components, all about 4 inches long but varying in diameter and weight. The variation in part geometries presented the greatest feeding challenge, while the need to switch between grinding wheels quickly made minimizing setup time between components equally critical to achieving the customer’s productivity and cost objectives.

Process
Glebar’s automated GT-610 Centerless Grinding System was selected to address the challenge of processing eight different part geometries in a single, continuous operation. The system was equipped with a 30-inch bowl feeder to accommodate the long tubes, with spouts oriented major diameter first to prevent feeding imbalances. Parts index as a single layer to the feeder discharge before transferring onto a conveyor vibratory inline system that carries them through the grinding wheel. An adjustable work rest blade, easily adjusted by turning a single screw via Glebar’s unique ramp device, allowed quick, accurate setup between the eight different components without the shimming required by competing methods. It met material removal requirements with a cycle time of about 10 parts per minute while holding a 0.0004-inch diameter tolerance.
Contact an EngineerSolution: Glebar GT-610 Centerless Grinder
The Glebar GT-610 Centerless Grinder’s 8-5/8-inch wide grinding wheel was ideally suited to the parts’ geometry, spreading material removal over a longer surface area for a more efficient grind and a superior surface finish than screw machines and other competing methods. A variable vibratory driver connected to the feeder plate controls part travel speed for consistent, reliable feeding throughout the cycle. The adjustable work rest blade eliminates the need for shimming, delivering faster, more accurate setup and improved roundness than conventional methods.