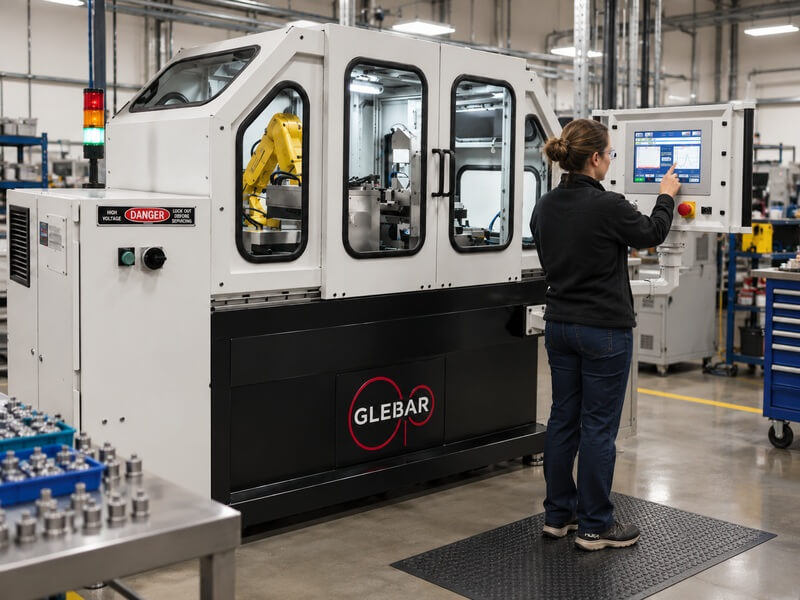
Burnishing Tools | Glebar GT-610 CNC
Challenge
The challenge was to develop a precision grinding solution for burnishing and expander rolls used in tube manufacturing across a wide range of industries, including oil and gas and automotive. These components have complex geometries with multiple tapers, requiring significant material removal across several operations and demanding both power and precision from the grinding system. Further complicating the process, the custom nature of each roll type requires reshaping the grinding wheel with every changeover between part configurations.
Process
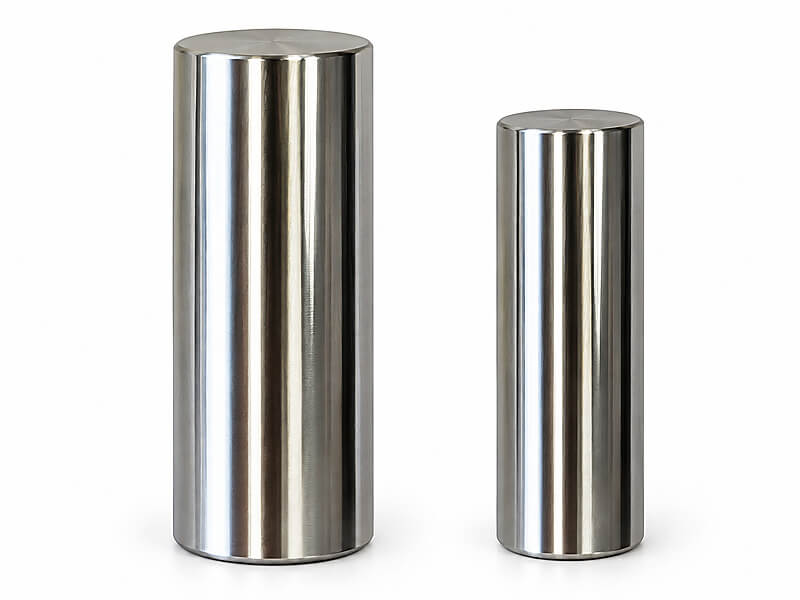
The existing operation was grinding 0.050” to 0.150” on a roughing pass, taking a maximum of 0.030” each pass until 0.005” of stock remained, and finish grinding 0.001”-0.002” per pass to maintain roundness, profile, and 10Ra surface finish on a large machine, overkill for a steel part that ranges from 0.250” to 1” in diameter. Changeover time was long, several grind setups were needed to grind 0.082” of material, and 4-5 passes were needed to achieve the required surface finish and roundness.
The GT-610-CNC Infeed/Thrufeed Centerless Grinder plunge grinds the part, maintaining 0.0001” diameter tolerance and the required shape –all in fewer passes. Removal of 0.082” takes only 113 seconds from start to finish, achieving 0.000025” roundness, with a 5 Ra surface finish, in only 3 total passes.
Contact an Engineer
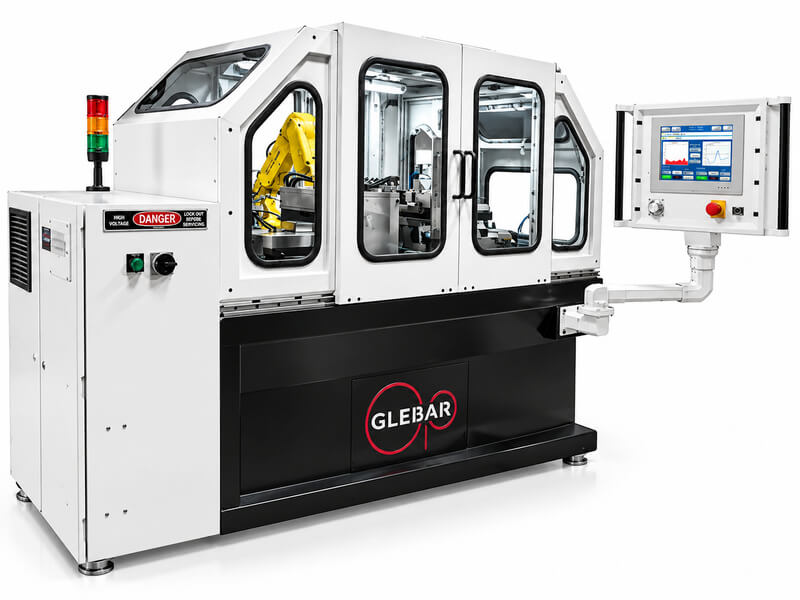
Solution: Glebar GT-610 CNC
The operator can switch between parts and operations by simply redressing the grinding wheel with the built-in CNC roll dresser. Alternatively, one can change to a pre-dressed grinding wheel in 15-20 minutes. The setup time is further reduced with the added patented lateral work rest blade axis, since full axis control is available with one touch on the touch screen control.